News

Top 10 Industrial Laser Cutter Types for Global Buyers

Choosing the right Industrial Laser Cutter is rarely a simple equipment decision. Material type, thickness, production volume, and available floor space all shape the answer. A machine that performs beautifully on stainless steel may struggle with thick acrylic or reflective aluminum. Real workshops reveal these differences quickly.

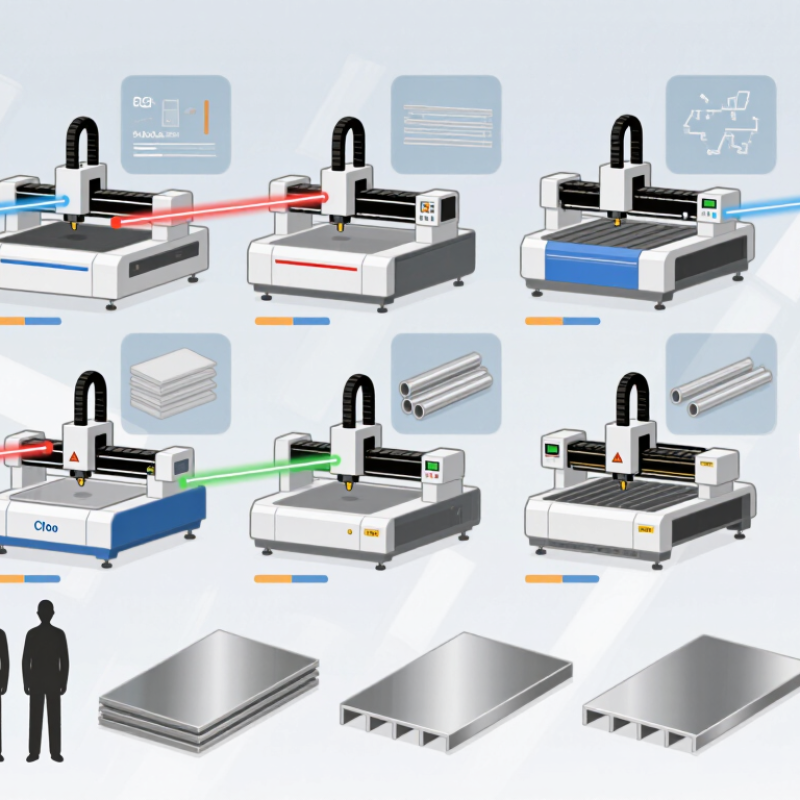
This guide examines ten major industrial laser cutter types used by global buyers. It compares fiber, CO2, diode, Nd:YAG, tube, sheet, three-dimensional, hybrid, precision, and automated systems. Each category has practical strengths and limitations. Cutting speed matters, but so do beam stability, nesting software, extraction systems, maintenance access, and operator training. A bright sample cut is not enough.

Look beyond the brochure.

Experienced purchasing teams should review sample-cut results, power requirements, service coverage, spare-part availability, and total ownership costs. They should also confirm safety features and applicable local standards before installation. Supplier claims deserve careful testing. Some figures depend on material grade, lens condition, assist gas, and factory temperature. This guide therefore focuses on usable comparisons rather than impressive specifications alone. It does not promise one universal winner. That would be misleading. Some comparisons remain imperfect, especially when manufacturers measure performance differently. Buyers should reflect on their actual workflow, not copy another factory’s setup. The best choice is usually the one that delivers consistent cuts, manageable downtime, and reliable support over many production cycles.
Top 10 Industrial Laser Cutter Types for Global Buyers

Industrial Laser Cutter Fundamentals and Classification Criteria

Industrial laser cutters are classified by laser source, output power, motion system, and material capability. The source determines wavelength, absorption, efficiency, and maintenance needs. Fiber systems suit reflective metals and thin-to-medium sheet. CO2 systems can process nonmetals and thicker materials effectively. Diode systems often provide strong electrical efficiency, but their application range can be narrower. These categories overlap in real factories. A machine’s label alone cannot predict its cutting quality.

Buyers should examine continuous power, peak power, spot size, beam quality, and assist-gas control. A smaller spot can produce finer details, yet it may reduce practical cutting speed. Bed size and axis design matter when handling a 3-meter steel plate. Flatbed, tube, and five-axis platforms serve different production geometries. Automation level also separates manual loading, shuttle tables, and robotic cells. Ask for sample cuts using your actual alloy and thickness.

Classification should include operating cost and risk control. Check energy use, consumable lenses, nozzle life, extraction performance, guarding, and service access. Safety systems need documented testing, not attractive promises. In my evaluations, vendors sometimes emphasize wattage while overlooking kerf stability and operator training. That is a weak comparison. No system is ideal. Dust, vibration, and imperfect material flatness can change results. A reliable decision combines measured trials, lifecycle data, and realistic production targets.
The Top 10 Industrial Laser Cutter Types Explained

The Top 10 Industrial Laser Cutter Types Explained

Industrial laser cutting is not one universal process. The practical choice depends on material, thickness, tolerance, and production volume. The ten main types are CO2, fiber, Nd:YAG, disk, diode, excimer, green, ultraviolet, picosecond, and femtosecond cutters. CO2 systems suit thick nonmetals and some steel. Fiber cutters usually handle sheet metal efficiently. Nd:YAG and disk lasers support demanding metal work. Diode systems offer lower energy use, while excimer, green, and ultraviolet lasers target delicate or reflective materials. Picosecond and femtosecond tools create extremely precise micro-cuts with limited heat damage.

Grand View Research estimated the global laser cutting machine market at about USD 5.7 billion in 2023. Its analysis also projects strong growth through 2030. The International Energy Agency reports that industrial electricity efficiency remains a major competitiveness issue. This makes beam quality and power consumption important buying factors. Still, the ranking is not absolute. A slower ultraviolet system may outperform a fiber cutter on brittle electronic parts. That detail is easy to miss.

Tips: Test the exact material before ordering. Measure edge roughness, kerf width, heat-affected zones, and cycle time. Review independent data sheets and maintenance records. Ask for sample cuts, not promises. A higher-power machine can waste energy when thin material dominates production. Conversely, choosing only by purchase price often creates hidden costs in optics, gas, extraction, and operator training.

Top 10 Industrial Laser Cutter Types for Global Buyers – The Top 10 Industrial Laser Cutter Types Explained

Rank Laser Cutter Type Typical Wavelength Typical Industrial Power Best-Suited Materials Typical Cutting Range Key Advantages Main Limitations
1 Continuous-Wave Fiber Laser Approximately 1,030–1,080 nm 1–30 kW Carbon steel, stainless steel, aluminum, brass, copper, galvanized sheet Thin sheet to approximately 40 mm steel, depending on power and process conditions High electrical efficiency, fast sheet cutting, compact optical path, low routine maintenance Reflective metals require suitable process settings; very thick sections may need slower cutting or alternative processes
2 CO₂ Laser Usually 10.6 μm; some systems operate near 9.3 μm 1–20 kW Carbon steel, stainless steel, acrylic, wood, plastics, textiles, rubber, glass and composites Thin materials to approximately 20–25 mm metal and substantially thicker nonmetallic materials Excellent performance on many nonmetals; mature technology; good edge quality on thick organic materials Lower wall-plug efficiency, larger beam-delivery system and more consumable maintenance than many fiber systems
3 Nd:YAG Laser Approximately 1,064 nm 0.5–6 kW continuous wave; lower average power for pulsed systems Steel, stainless steel, aluminum, nickel alloys, titanium and selected reflective metals Approximately 0.1–10 mm for common industrial cutting applications Good focusability and compatibility with fiber delivery; suitable for precision cutting and welding Generally less energy-efficient and more maintenance-intensive than modern fiber sources
4 Thin-Disk Laser Approximately 1,030–1,080 nm 2–16 kW Carbon steel, stainless steel, aluminum, copper, brass and high-strength alloys Thin sheet to approximately 25–30 mm steel in suitable high-power configurations High beam quality at high power, good thermal management and strong performance in demanding industrial production More complex and expensive architecture; specialist servicing may be required
5 Direct-Diode Laser Approximately 800–1,000 nm 1–20 kW Copper, brass, aluminum, stainless steel, coated metals and selected polymers Thin sheet to approximately 10–15 mm metal, depending on beam quality and power High electrical efficiency and strong absorption in some reflective metals; simple solid-state design Beam quality can be lower than fiber or disk lasers, which may limit very fine kerf work
6 Pulsed Fiber Laser Approximately 1,030–1,080 nm 20–1,000 W average power; high peak power in short pulses Thin stainless steel, nickel alloys, titanium, aluminum, copper, foils and precision components Foil and thin sheet, commonly below approximately 3 mm Low heat input, narrow kerf, precise edge control and excellent suitability for small or delicate parts Slower or unsuitable for heavy plate; process quality depends strongly on pulse width and frequency
7 Ultraviolet Solid-State Laser Commonly 355 nm; other harmonics are also used 5–100 W for many industrial micromachining systems Polymers, ceramics, glass, thin metals, electronics materials, films and medical components Micromachining applications from films and foils to approximately 1 mm, depending on material Small heat-affected zone and efficient absorption in many nonmetallic materials; high detail resolution Lower power and higher source cost; optics and process conditions require careful control
8 Excimer Laser Approximately 193–351 nm, depending on the gas mixture Typically tens to several hundred watts average power Polymers, thin films, semiconductor materials, ceramics and specialized medical or optical materials Micron-scale features, thin films and thin sheets rather than heavy plate Cold ablation, very fine features and low thermal damage on suitable materials Gas handling, optical maintenance and higher operating complexity; limited general-purpose metal cutting
9 Ultrafast Laser Commonly 1,030 nm, 515 nm or 343 nm 10–500 W average power with picosecond or femtosecond pulses Glass, ceramics, sapphire, polymers, composites, thin metals and brittle materials Microfeatures, thin sheets and precision holes; commonly below approximately 2 mm Minimal heat-affected zone, high dimensional accuracy and clean processing of difficult materials High purchase cost, lower throughput for large sections and demanding beam-delivery requirements
10 Green Laser Approximately 515–532 nm 10–500 W, depending on continuous-wave or pulsed design Copper, brass, gold, silver, aluminum, thin foils and reflective electronic materials Foil and thin sheet, commonly approximately 0.05–3 mm Improved absorption in copper and other reflective metals; precise, low-spatter processing Lower available power and higher system complexity than mainstream infrared fiber cutting systems

Note: Power and thickness figures are representative industrial ranges rather than guaranteed specifications. Actual performance depends on material grade, reflectivity, assist gas, focal optics, cutting speed, part geometry and machine configuration.

Cutting Materials, Applications, and Performance Differences

Top 10 Industrial Laser Cutter Types for Global Buyers

Fiber laser cutters lead metal processing because they deliver high speed, narrow kerfs, and strong energy efficiency. They handle carbon steel, stainless steel, aluminum, brass, and copper. CO2 cutters remain useful for acrylic, wood, rubber, textiles, and thicker nonmetal sheets. Nd:YAG systems suit detailed metal work, welding preparation, and reflective surfaces, although maintenance can be demanding. Disk lasers provide high power with stable beam quality for heavy steel plates. Diode lasers offer efficient surface treatment and moderate cutting, but their edge quality may vary.

Excimer lasers work with ultraviolet wavelengths and serve delicate polymers, films, and specialized electronics. UV laser cutters create fine details on glass, ceramics, plastics, and coated materials with limited heat damage. Green lasers interact effectively with copper, gold, and other reflective metals. Ultrafast picosecond and femtosecond systems produce extremely precise cuts in brittle or heat-sensitive parts. Tube laser cutters use rotating fixtures to process pipes, profiles, and structural sections from several angles.

Application changes the best choice. A fiber system may outperform CO2 on steel, while CO2 can produce cleaner acrylic edges. Cutting speed depends on thickness, assist gas, nozzle design, and thermal control. Power alone is not enough. A polished sample can mislead. Real production tests should measure burrs, taper, warping, cycle time, and operating cost. I have seen buyers overlook loading accuracy, then blame the laser for inconsistent tube cuts. That mistake is expensive. Evaluate material mix, tolerances, service skills, and future capacity before selecting equipment.

How to Choose the Right Industrial Laser Cutter

Top 10 Industrial Laser Cutter Types for Global Buyers

How to Choose the Right Industrial Laser Cutter

Choosing an industrial laser cutter starts with the material, not the advertised power. Fiber systems suit steel, stainless steel, aluminum, and many reflective metals. CO2 systems can handle acrylic, wood, plastics, and other nonmetal materials. For specialized work, crystal and hybrid systems may offer useful flexibility. However, the wrong source can increase heat damage, waste, and maintenance costs.

Measure your real production needs. Record material thickness, sheet size, daily cutting hours, required tolerance, and average batch volume. A 6,000-watt machine may cut thick steel quickly, but it can be excessive for thin parts. Higher power is not always better. It may raise energy use and reduce financial efficiency. Check acceleration, pierce time, nesting software, and automatic loading features. Small gains become significant during long shifts.

Safety and service deserve equal attention. Look for enclosed working areas, fume extraction, interlocks, emergency controls, and documented operator training. Ask whether replacement optics, lenses, and filters are available in your region. Review installation requirements, including power quality, cooling, ventilation, and floor strength. Remote support sounds convenient, but local technicians often solve problems faster. A purchasing team should request sample cuts using its own materials. Even then, results can change with nozzle wear, gas purity, and operator settings. That uncertainty needs to appear in the budget.

Global Purchasing Factors, Safety Standards, and Maintenance Needs

For global buyers, comparing ten laser cutter types means matching material, thickness, duty cycle, and service access. Fiber, CO2, Nd:YAG, disk, diode, UV, green, excimer, picosecond, and femtosecond systems behave differently. Fiber units usually cut sheet metal quickly and use less alignment-sensitive optics. CO2 machines remain useful for many nonmetals, but mirrors and gas paths demand stricter upkeep. UV and ultrafast machines suit delicate work, yet their purchase and calibration costs can rise sharply. The World Robotics 2024 report recorded 541,302 industrial robot installations worldwide in 2023, up 2 percent. That growth makes interface compatibility and guarded automation practical buying factors, not decorative features.

Safety must be verified before price. IEC 60825-1 classifies laser products, while ISO 11553-1 addresses laser-processing machine safety. ANSI Z136.1 offers widely used exposure-control guidance, but local rules still govern installation and training. Enclosures, interlocks, emergency stops, fume extraction, and beam alignment procedures need documented tests. The U.S. Bureau of Labor Statistics reported 2.6 million nonfatal private-industry injuries and illnesses in 2023. This figure is not laser-specific, yet it challenges the lazy assumption that a closed machine is automatically safe.

Maintenance planning should include lens cleaning, nozzle inspection, chiller checks, filter replacement, grounding tests, and software backups. Ask suppliers for measured uptime, spare-part lead times, technician response, and preventive-maintenance schedules. Track kerf width, edge oxidation, power stability, and cutting-gas pressure each shift. Small drift becomes expensive scrap. Costs compound. Published market reports often emphasize sales growth, not lifetime service costs. Buyers should request local service records and calculate energy, consumables, downtime, and disposal costs over five years.

Top 10 Industrial Laser Cutter Types for Global Buyers

Representative laser emission wavelengths are shown below. Actual performance depends on laser power, optics, assist gas, material, and cutting-head configuration.

Global purchasing factors: Buyers should evaluate material range, rated power, cutting speed, automation compatibility, electrical requirements, local service capability, spare-parts availability, and total cost of ownership.

Safety and maintenance: Enclosed systems should be assessed against applicable laser-safety requirements such as IEC 60825-1 and machine-safety requirements such as ISO 12100. Routine needs commonly include lens and window inspection, nozzle alignment, assist-gas filtration, cooling-system checks, exhaust maintenance, calibration, and preventive replacement of wear parts. Open-beam systems require controlled access, interlocks, beam enclosures, and wavelength-appropriate protective eyewear.